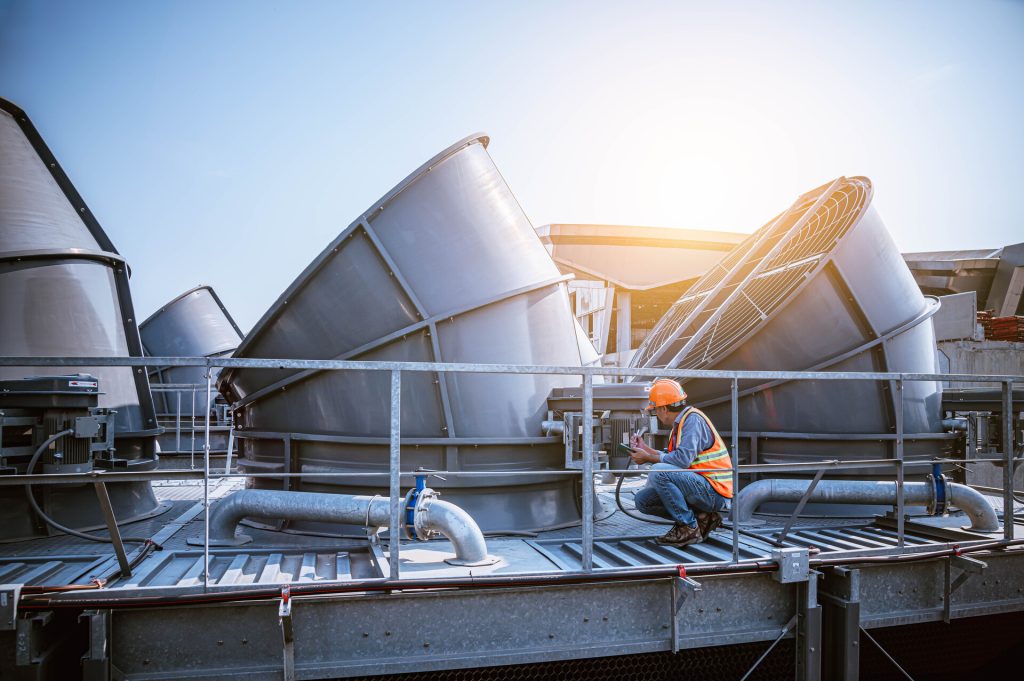
Cooling towers operate under stress that few other systems experience: warm, nutrient-rich water constantly recirculates through metal surfaces while being exposed to air and sunlight. This environment is hostile to equipment and favorable to biological growth. Left untreated, cooling towers fail through five distinct mechanisms, each accelerating the others. A system can appear to function normally while degrading invisibly — until catastrophic failure forces shutdown and emergency repair. The alternative is straightforward: proper water treatment prevents all five failure modes simultaneously and costs far less than emergency restoration.
01 — The EnvironmentWhy Cooling Towers Are Uniquely Challenging
Cooling towers operate in conditions that concentrate chemical and biological stressors. Recirculating water increases mineral concentration through evaporative loss (cycles of concentration can reach 3–5× makeup water hardness). Warm water temperatures (95–120°F) accelerate chemical reactions and promote biological growth. Open-air exposure introduces dissolved oxygen and airborne contaminants. Metal heat exchangers and piping become electrodes in this corrosive environment. The cumulative effect is a system that requires active chemical management or it will degrade rapidly.
This degradation is not dramatic or sudden. It is insidious. A cooling tower can lose 10–20% of heat transfer efficiency per year through scale and fouling while appearing to operate normally. Energy costs rise, chiller run time increases, and equipment life shortens — all invisible to operators until failure forces investigation.
Five Failure Modes That Cascade When Untreated
02 — Scale FormationThe Invisible Efficiency Killer
Scale forms when hardness minerals (calcium and magnesium) precipitate out of solution and adhere to heat transfer surfaces. The tendency to form scale increases with temperature, pH, and cycles of concentration. Scale is an insulator — even a thin layer dramatically reduces heat transfer efficiency. A 1mm layer reduces heat transfer by 10–15%; a 3mm layer by 30–40%. The result is higher chiller run time, increased energy costs, and accelerated equipment wear.
Scale is particularly dangerous because it is often invisible in early stages. The system continues operating, but at declining efficiency and rising cost. By the time scale buildup becomes visible (typically 2–5mm thickness), the tower has already lost significant capacity and efficiency may not be fully recoverable without chemical cleaning or mechanical descaling.
Threshold inhibitor chemistry (typically polymeric or phosphate-based) prevents scale crystal nucleation and growth at the molecular level. These compounds interfere with crystallization without completely removing hardness from the water, allowing higher cycles of concentration without scale formation.
How It Works- Inhibitor adsorbs onto nascent hardness crystals
- Blocks further crystal growth and precipitation
- Allows cycles of concentration up to 4–6× makeup water hardness
- Lower chemical cost than full water softening
- CI 98 Cooling Water (polymeric inhibitor)
- CI 87 Cooling Water (alternative formulation)
- Both formulated with corrosion inhibitors for multi-protection
- Prevents scale formation at normal operating cycles
- Maintains heat transfer efficiency at baseline levels
- Typical cost: $1,000–$3,000 annually depending on system size
Once scale has accumulated, prevention alone is insufficient. Chemical descaling must dissolve existing deposits. This requires chelating or acidic chemistry to hydrolyze mineral bonds and suspend scale particles for removal. Descaling is expensive and requires system downtime.
How It Works- Acidic or chelating compound dissolves mineral deposits
- Sustained contact time (12–48 hours typically) required
- System circulation maintains chemical contact with all surfaces
- Requires careful pH control to prevent corrosion during treatment
- Expensive: $5,000–$20,000 depending on scale severity
- Requires system shutdown and downtime
- Corrosion risk if not executed properly
- Preventative treatment costs far less
- Proper inhibitor treatment prevents 95%+ of scale formation
- Avoids costly emergency descaling and shutdown
- Maintains efficiency continuously
03 — CorrosionThe Silent Infrastructure Destroyer
Corrosion in cooling towers is electrochemical: oxygen, chlorides, and pH variations initiate oxidative attack on steel, copper, and aluminum surfaces. Unlike scale, which is visible, corrosion often occurs beneath sludge and biofilm layers. Under-deposit corrosion creates pits that concentrate stress and lead to unexpected tube failure and leaks. By the time corrosion becomes visible (through rust staining or leakage), significant metal loss has already occurred.
Different metals corrode at different rates and through different mechanisms. Steel corrodes through oxygen-driven attack. Copper corrodes through oxidation and can initiate secondary corrosion in steel through galvanic coupling. Aluminum is amphoteric — it corrodes in both acidic and highly alkaline conditions. Proper corrosion inhibitor treatment protects all metals simultaneously.
04 — Biofilm & Microbial FoulingThe Growth That Never Stops
Cooling towers provide the perfect environment for bacteria, algae, and fungi: warm water, nutrients from makeup water contamination, aeration, and often stagnant zones. Biofilm forms within days if left untreated. Once established, biofilm is extremely difficult to remove and creates secondary problems: it insulates surfaces (like scale), reduces heat transfer, harbors pathogenic organisms, and creates anaerobic pockets where corrosion accelerates.
Legionella pneumophila, the bacterium responsible for Legionnaires' disease, proliferates in untreated cooling towers. Legionella outbreaks have caused building closures lasting months and created substantial liability. Biocide treatment is not optional — it is a regulatory requirement in many jurisdictions and a health and safety imperative.
Continuous biocide feed maintains microbial suppression as makeup water introduces new organisms. Low-dose continuous treatment prevents biofilm buildup and is often more cost-effective than periodic shock dosing. Glutaraldehyde-based biocides are effective against slime-forming and sulfate-reducing bacteria.
Mechanism- Continuous low-dose (typically 1–3 ppm residual)
- Prevents biofilm attachment and growth
- Suppresses pathogenic Legionella amplification
- Often combined with oxidizing biocide (chlorine/bromine)
- CI Gluticide 15 (glutaraldehyde-based)
- CI B-10 Biocide (bronopol-based)
- Both applicable as continuous feed or slug dose
- Prevents biofilm accumulation on heat surfaces
- Maintains heat transfer efficiency
- Reduces Legionella risk substantially
When biofilm has already accumulated (typically visible as slime on surfaces or reduced water clarity), higher-dose slug applications are required to penetrate and kill established biofilm. Shock dosing is more aggressive than continuous treatment but may be necessary if microbial problems are already visible.
Mechanism- Higher biocide concentration (10–30 ppm)
- Applied as single dose, held in circulation
- Penetrates biofilm matrix and kills bacteria
- Requires 4–8 hours contact time typically
- Visible slime on surfaces or piping
- Biofilm preventing heat transfer
- Legionella risk assessment indicates contamination
- Monthly or quarterly supplemental treatment
- More expensive per application than continuous dosing
- Typically 4–12 applications per year
- Combined cost lower than continuous if system is well-maintained
05 — Operational ConsequencesWhat Untreated Cooling Towers Cost
The cumulative effect of scale, corrosion, and biofilm is predictable: declining heat transfer efficiency, rising energy consumption, increased equipment wear, and eventually failure. A cooling tower operating at 70% of design capacity (which often goes undetected) costs 20–30% more in energy annually. Over a 20-year equipment life, untreated cooling towers cost $500,000–$2,000,000+ in excess energy consumption and premature equipment replacement.
Scale and fouling reduce heat transfer efficiency by 2–5% annually. Over 10 years, untreated tower may consume 25–50% more energy than properly maintained system. Annual energy cost increase: $20,000–$100,000 depending on facility size.
Corrosion, scale-induced stress, and biofilm damage reduce chiller and heat exchanger lifespan from 20–25 years to 8–12 years. Premature replacement cost: $200,000–$1,000,000 depending on equipment capacity.
Cooling system failure forces facility shutdown. Loss of productivity, emergency repair costs ($50,000–$500,000), and emergency service premiums create substantial financial impact in addition to operational disruption.
Legionella outbreak in untreated cooling tower can close facility for months, create staff/customer health crisis, and expose organization to regulatory fines and lawsuit liability ($1,000,000+).
Many jurisdictions require documented cooling tower treatment programs and Legionella risk assessments. Untreated systems create compliance violations and regulatory enforcement action.
Without proper inhibitor treatment, cycles of concentration must be kept low to prevent scale. This requires more frequent blowdown and higher makeup water consumption, increasing operating costs 15–25%.
06 — Comprehensive Treatment ProgramThe CI Cooling Tower Solution
| Treatment Component | Primary Function | Product Example | Frequency / Dosage |
|---|---|---|---|
| Scale Inhibitor | Prevents hardness mineral precipitation on heat surfaces | CI 98 Cooling Water or CI 87 Cooling Water | Continuous feed; typically 2–5 ppm residual maintained |
| Corrosion Inhibitor | Protects ferrous, copper, and aluminum from electrochemical attack | Included in CI 98 and CI 87 formulations | Combined with scale inhibitor; no separate dosing |
| Non-Oxidizing Biocide | Kills slime-forming and sulfate-reducing bacteria | CI Gluticide 15 (continuous or slug dose) | Continuous: 1–3 ppm; Slug: 15–25 ppm monthly/quarterly |
| Alternative Biocide | Fast-acting microbial control, broad-spectrum efficacy | CI B-10 Biocide (bronopol-based) | Continuous or slug dose; may be rotated with CI Gluticide 15 |
| Oxidizing Biocide (Optional) | Supplemental Legionella control; works synergistically with non-oxidizing biocide | Chlorine or bromine (external supply) | 0.5–1.0 ppm residual; often used 2–3x weekly |
| pH Buffer / Alkalinity | Maintains pH in target range (7.5–8.5); prevents corrosion and scale formation | Sodium carbonate or alkalinity booster | As-needed based on water test results |
Five Steps to Building Your Cooling Tower Protection Program
- Water Analysis Baseline: Test makeup water hardness, alkalinity, pH, iron, and copper. Establish baseline chemistry and identify initial treatment needs. Repeat annually to detect changes in water source.
- Inhibitor Program: Deploy continuous-feed scale and corrosion inhibitor (CI 98 or CI 87) to maintain baseline heat transfer efficiency and prevent new scale formation. Cost: $1,000–$3,000 annually.
- Biocide Strategy: Establish continuous (low-dose) or periodic (high-dose shock) biocide treatment using CI Gluticide 15 or CI B-10. Frequency depends on water quality and biofilm history. Cost: $1,500–$4,000 annually.
- Monitoring Program: Conduct monthly water testing (residual inhibitor, pH, alkalinity, microbial indicators). Track results and adjust treatment as needed. Monthly testing enables early detection of problems.
- Documentation & Compliance: Maintain detailed records of all treatment applications, water test results, and maintenance history. This documentation protects warranty, demonstrates regulatory compliance, and guides future service decisions.
Cooling towers don't announce when they're failing. They just slowly lose efficiency while energy costs climb, corrosion accelerates invisibly, and biofilm spreads. By the time failure becomes obvious, the damage is done. The facilities that remain efficient and avoid catastrophic failure are not the ones with fancy equipment — they are the ones with disciplined water treatment. Chemistry prevents 95% of cooling tower problems. The other 5% cost millions to fix.
CI Water Treatment — Cooling Systems Series
Ready to Protect Your Cooling Tower?
Chem International's cooling water specialists can conduct a baseline water analysis of your system, recommend a customized inhibitor and biocide program, and establish a monitoring protocol to keep your cooling tower operating at peak efficiency while preventing scale, corrosion, and biological fouling.
Contact CI Cooling Water Specialists